Broach design turns a finished part requirement into a sequence of cutting edges. Each edge has a defined position and geometry, so the designer must consider the starting shape, material removal, chip space and machine limits together. A workable design is a coordinated cutting plan, not simply a drawing of the final profile.
Table of Contents
- What Broaches Must Accomplish
- Start With the Workpiece and Machine
- Choose the Broach Configuration
- Plan the Cutting Sequence and Rise per Tooth
- Set Tooth Pitch and Gullet Capacity
- Choose Tooth Geometry and Tool Material
- Check Force, Stroke and Tool Strength
- Document, Manufacture and Verify the Tool
- Frequently Asked Questions
- Discuss Your Broaching Application
- References
This guide follows an internal pull broach as a reference case. Surface and other broaches use different arrangements, but the same questions about stock, chip formation, force and inspection help frame their design. A tool specialist should verify the final geometry against the actual part and machine.
Key takeaways
- Start with the finished profile, starting stock and machine envelope.
- Check tooth rise, pitch and gullet capacity together as the cutting sequence develops.
- Verify force, stroke, holding and inspection before approving the tool drawing.
What Broaches Must Accomplish
A broach removes stock through a series of teeth. The difference in height between successive cutting edges is the rise per tooth; the distance between teeth is the pitch. Chips form at the cutting face and must fit in the space, or gullet, ahead of the tooth. Kokturk's thesis explains how these features interact with the cutting process and the finished surface.
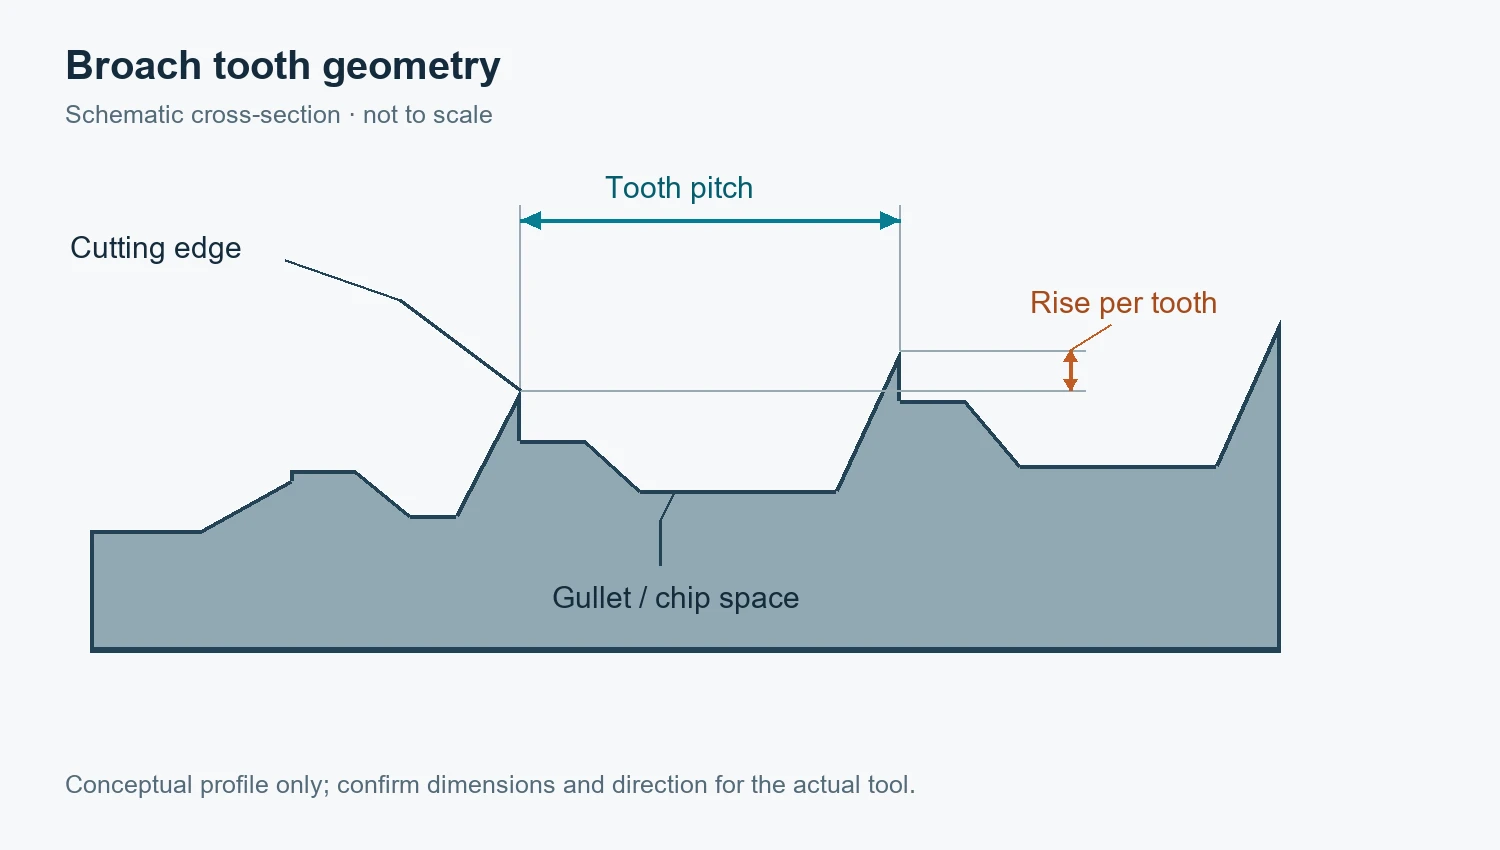
A useful design therefore has several jobs at once:
- Guide the tool into and through the workpiece without losing alignment.
- Distribute the stock across cutting teeth while controlling load and chip formation.
- Provide sufficient space for chips throughout the cut.
- Bring the profile to its specified size and finish with appropriate finishing teeth.
- Fit the available machine stroke, force, holders and workholding.
These jobs can compete. For example, changing pitch changes both the spacing of engaged teeth and the space available for chips. It can also change the length of the tool. The design should be reviewed as a system rather than by choosing each feature independently.
The article on broach manufacturing provides a related view of the production route after the design has been specified.
Start With the Workpiece and Machine
The first design input is the part drawing. Identify the final profile and its tolerances, the datum surfaces that locate it, the length of material being cut and any entry or exit restrictions. For an internal broach, record the starting hole dimensions and their variation as well as the final profile. A drawing that gives only the finished size leaves the designer unable to establish the actual stock to be removed.
Material condition matters as much as material name. Obtain the specified grade, hardness or heat-treatment condition, and any relevant variation between batches. Kokturk's thesis describes how workpiece material, tool geometry and cutting conditions influence the process; a geometry selected for one material should not automatically be transferred to another.
Next establish the operating envelope. Record available stroke, rated force, holding arrangement, fixture location, clearance and coolant provision. Check how the broach enters and leaves the part, including the space occupied by pilots and the pull end. If the tool cannot complete its travel with the part securely located, a theoretically suitable tooth layout is not a usable design.
The following input table turns those requirements into a review list for the toolmaker:
| Input | What to establish | Design decision affected |
|---|---|---|
| Part profile and starting opening | Dimensions, tolerances and datums | Stock distribution and final tooth profile |
| Workpiece | Grade, hardness and condition | Cutting geometry and tool material selection |
| Cutting length | Material traversed by a tooth | Pitch, tooth engagement and chip storage |
| Machine and fixture | Force, stroke, interfaces and clearance | Tool length, connection and support |
| Inspection | Profile measurement and acceptance criteria | Finishing and verification plan |
A practical input sheet should also include production volume, inspection method and the condition of the incoming blank. These affect choices such as tool construction, expected reconditioning and the amount of process verification needed before production. Mark missing values as open questions and resolve them with the part owner or machine operator before approving the tool drawing.
Choose the Broach Configuration
Select the configuration from the shape and access of the feature. An internal broach passes through an existing opening to produce an internal form; a surface broach cuts an external surface. The tool may be made as one body or as a sequence of sections, depending on the profile, stock and available equipment.
For an internal pull broach, the pull end connects the tool to the machine, the front pilot helps guide it into the starting opening, and the cutting section follows. A rear pilot can support alignment as the final teeth pass through. The actual arrangement must match the machine holder and the workpiece geometry; these names alone do not specify the dimensions of a tool.
Kokturk's thesis discusses tools composed of segments with different profiles. This provides a design alternative when a single tool would exceed the machine envelope. The handoff between operations must still preserve location and leave a defined intermediate shape.
Choose a cutting strategy before detailing individual teeth. Decide which portions of the profile are cut at each stage, whether the profile is generated progressively, and which surfaces are left for finishing. For complex forms, the section being removed changes from tooth to tooth. Özlü and colleagues describe a simulation approach that generates intermediate tooth shapes and evaluates forces for complex broach geometry.
Plan the Cutting Sequence and Rise per Tooth
Divide the working section into roughing, semi-finishing and finishing functions. Roughing teeth remove the bulk of the stock; later teeth bring the profile toward its final form. Reserve or calibration teeth may have no additional rise. The rise should be selected for the workpiece and assigned to the appropriate cutting section.
The starting stock and selected rise determine how much work is assigned along the tooth sequence. A larger rise can reduce the number of cutting teeth needed for a given amount of stock, but it changes the load on the edge and the volume of the chip. A smaller rise may reduce the load per tooth while increasing the length of the cutting section. The final choice depends on material, profile, tool strength and the available machine stroke.
Work from the worst permitted starting condition rather than a nominal value alone. If the starting opening varies, the first working teeth must accommodate that variation without creating an unintended overload. The designer should also allow for the required finished profile and the role of the finishing section. For a non-round profile, check stock around the complete contour: different portions may not remove material at the same rate.
Rise per tooth is built into the relationship between the edges of a conventional fixed-geometry broach. Changing cutting speed changes an operating condition, but does not by itself change that geometric rise. If the planned rise is unsuitable, review the cutting strategy or tool geometry with the tool designer rather than treating machine speed as a substitute for redesign.
Set Tooth Pitch and Gullet Capacity
Pitch determines how teeth are spaced along the tool. Cutting length and the number of teeth engaged at once are central inputs. Kokturk's thesis relates pitch and gullet geometry to the chip-storage calculation. A pitch that leaves too few teeth cutting can make engagement less stable; adding teeth to the cut also changes total force.
The gullet must hold the chip produced during the passage through the workpiece. Its usable capacity is affected by its shape and by how the chip curls and packs. A longer cutting length or a larger rise can increase the chip volume that a tooth must carry. The relationship is particularly important in internal work, where the chip remains in the gullet until the tooth exits.
Köktürk's broach-design thesis uses a chip-volume-to-gullet-volume limit of 0.35 in its optimization method. This is a design criterion within that method, not a replacement for a toolmaker's assessment of chip shape and the actual application. The calculation is useful because it forces the designer to check chip storage explicitly instead of assuming that any space between teeth is sufficient.
A pitch and gullet review should answer three separate questions: will the required number of teeth engage, can each gullet accommodate its chip, and will the resulting tooth and tool length fit the machine? A proposed change should be checked against all three. If the gullet check fails, changing the cutting plan, pitch or tool sequence may be more appropriate than increasing cutting force to push chips through.
Choose Tooth Geometry and Tool Material
The rake face directs chip formation, while relief behind the cutting edge helps prevent the tool from rubbing on the newly machined surface. Tooth geometry must be chosen for the workpiece and cutting conditions, not copied from a generic drawing. Köktürk's thesis discusses rake and clearance angles alongside pitch, rise and force in its treatment of broach design.
The shape of the tooth root and gullet also affects the material left to support the cutting edge. A deeper or wider chip space can improve storage but changes the tooth cross-section. The designer must check the edge and root for the expected cutting loads and consider how the tool will be manufactured and sharpened.
Finishing and roughing teeth need not have identical geometry. Their jobs differ: one group removes more stock, while the finishing group controls the final surface and size. Land and relief details should be specified in a way that supports the intended regrinding method. The drawing should identify which faces may be reground and which dimensions must remain controlled after reconditioning.
Tool material and any coating are selected with the workpiece, cutting conditions, production requirement and maintenance route in mind. Tool material selection should be reviewed together with the proposed cutting geometry. A material label alone does not establish tool life: the cutting edge, heat treatment, geometry, lubrication and operating conditions must be evaluated together.
Check Force, Stroke and Tool Strength
A machine must carry the combined load of the teeth in contact at the same time. Estimating force for one tooth is therefore only part of the check: the engagement pattern, cutting width, rise and workpiece material affect the total. The force prediction should be compared with the machine rating and with the limits of the pull connection, tool body, fixture and workpiece support.
Köktürk's thesis models cutting force using cutting coefficients, width and uncut chip thickness, with a separate edge-force component. The model illustrates why force estimates depend on coefficients appropriate to the material and process. If those coefficients are uncertain, record the assumption and use a suitable engineering margin rather than presenting a calculation as a measured result.
Also check the complete travel. The cutting section, pilots and connection occupy length, and the tool must enter and leave the workpiece with the fixture in place. A force-compliant design can still be unsuitable if it exceeds stroke or interferes with the machine. Review the tool at entry, full engagement and exit, not only at a single drawing position.
For long or slender tools, the direction of loading and support arrangement deserve particular attention. Pulling and pushing place different demands on the tool body. Check the relevant sections for the applied load and avoid assuming that the rated machine force guarantees adequate tool strength. The part fixture must resist the process load without allowing movement that changes the profile or damages the tool.
Document, Manufacture and Verify the Tool
A useful working drawing communicates more than the final profile. It identifies the connection, pilots, cutting and finishing sections, tooth geometry, material and heat-treatment requirements, critical dimensions and inspection references. The design record should also preserve the assumed starting stock, material condition, cutting length and machine constraints so that a future change can be evaluated against the original basis.
Before manufacture, review the drawing with the people responsible for toolmaking, setup and inspection. Confirm that the geometry can be produced and measured, that the holder and fixture interfaces match, and that the specified regrinding surfaces are accessible. If a feature cannot be inspected by the planned method, agree on an alternative before accepting the drawing.
During the first controlled run, check the starting part, the setup and the actual operating conditions against the design inputs. Observe chips and look for packing, damaged edges or unusual marks. Measure the produced profile against the drawing and record where measurements were taken. A process that reaches size once should still be checked for consistency over the agreed sampling plan.
If the result is outside requirements, isolate the cause before changing several variables together. Verify the incoming stock and location, inspect tool condition and holder alignment, then compare operating conditions with the approved plan. Chips, force behaviour and the location of marks can help guide the investigation. Keep the original inspection results and document each change so that a later run can be compared meaningfully.
The related guide to broach tool inspection covers inspection considerations beyond the initial design review. A maintenance plan should define when to inspect and how regrinding will be approved for the particular tool.
Frequently Asked Questions
Can one broach design be used for several parts?
It can be considered when the parts share the required profile and the full range of starting stock, material condition, cutting length and machine interfaces fits the design. Compare the limiting case for each input with the tool drawing. A shared final dimension alone is insufficient to establish interchangeability.
What should be supplied when requesting a custom broach?
Provide the part drawing, starting shape and tolerance, material condition, cutting length, machine force and stroke, holder details, production requirement and inspection method. Include a sample or fixture drawing when available. Identify any unknowns so the supplier can resolve them before committing to a geometry.
When should a broach be redesigned instead of reconditioned?
Reconditioning addresses the approved tool's condition within its specified maintenance limits. A change to material, starting stock, profile, machine or production requirement may alter the design basis. Compare the new conditions with that basis and ask the tool designer to assess the remaining geometry and strength before reuse.
Discuss Your Broaching Application
A sound broach design starts with a complete part and machine specification, then checks the cutting sequence, chip storage, force and inspection plan together. If you need help reviewing the application or matching a tool and machine, contact the BroachingMach team. Share the drawing and operating constraints so the discussion can begin with the actual job.
References
- Optimization of Broaching Tool Design — Köktürk's thesis on gullet capacity, cutting force and tool optimization.
- Broaching tool design through force modelling and process simulation — Özlü and colleagues describe force modelling and intermediate tooth geometry.