Most failures in a broaching operation come from five areas that a technician can check in order: tooth engagement, edge and fluid condition, chip space, measured capability of the feature, and the machine's ram, slideways and hydraulics. Start with the checks that cost nothing, such as counting engaged teeth and measuring a sample. Move to regrinding or a fluid change only when those checks point there. Leave machine repair for last.
This guide is for production engineers and maintenance technicians who run pull or push broaching on internal holes, splines and keyways. It covers surface defects, dimensional drift, stalls and broken teeth, and machine-side faults in slideways and hydraulics. It does not cover electrical or control faults or CNC single-point broaching. For polygon forms cut on lathes and mills, see our guide to rotary broaching troubleshooting.
Each section lists the symptom, the checks in the order to run them, and the published evidence behind the check. The checks are conditional: a result tells you which branch to follow, not what to buy or regrind.
Key takeaways
- Count the teeth in the cut before touching speed. Handbook practice sizes the pitch so that two or more teeth cut at once.
- A fluid change can move surface finish and tool wear. In one published test, a 5% emulsion wore the broach quickly, while a 15% emulsion held the drawing's roughness limit.
- Compare Cm with Cmk on a 50-piece sample before blaming the tool. A large gap between them points to centering, not spread.
- Chip packing is a tool-design and cleaning problem first. Round broaches without chipbreakers can wedge ring-shaped chips in the gullets.
- Hydraulic noise that sounds like gravel points first to the pump inlet: oil level, inlet piping and the intake screen.
Table of Contents
- Broaching troubleshooting: three facts to collect first
- Broach chatter in a broaching operation: tooth engagement and rigidity
- Torn, rough or burred surfaces: edge condition and cutting fluid
- Out-of-tolerance features and gauge failures: tool, machine or process
- Stalls, chip packing and broken teeth
- Uneven ram motion and slideway friction
- Hydraulic pressure loss, noise and aeration
- Frequently Asked Questions
- Send us the failure details
Broaching troubleshooting: three facts to collect first
Before changing anything, write down three facts. First, what the defect looks like and where it sits on the part. Second, when it started: the first part of a batch, mid-run, or after a tool change. Third, what changed last: a material lot, a regrind, a fluid top-up or a machine repair.
These three facts matter because many things can shift a process at once. In their study of broached impeller hubs, Martinovic and Peterka list the usual sources of variation in capability measurements: machine (including tool wear and tooling choice), measurement, operator, material, environment and method. A defect that appears right after one of these changed is a stronger lead than any general rule.
The table below maps a symptom to the first check. Details and the evidence for each check follow in the sections after it.
| Symptom | First check | Section |
|---|---|---|
| Fish-scale marks, growl, erratic size along the cut | Teeth in the cut, then clamping and tool mounting | Chatter |
| Torn walls, rough finish, heavy burrs | Edge condition, then fluid concentration and delivery | Surface defects |
| Go-gauge binds, no-go passes, feature drifts | Capability sample, then entry, middle and exit readings | Tolerance |
| Stall mid-stroke, snapped or chipped teeth | Chips in the gullets, then load against machine capacity | Stalls and breakage |
| Ram hesitates or crawls | Slideway film, then hydraulic condition | Ram motion |
| Falling force, knocking pump | Oil level, inlet piping, intake screen | Hydraulics |
Broach chatter in a broaching operation: tooth engagement and rigidity
Symptom. Fish-scale or cross-hatch marks on the broached surface, a rhythmic knock during the stroke, and size that varies along the cut.
What the literature says. Schneider's handbook chapter on broaches states that pitch is calculated so that, preferably, two or more teeth cut at the same time, and that this keeps the tool from drifting or chattering. The same chapter says broach designers may set the teeth at a shear angle to improve surface finish and reduce chatter. Both are design features of the tool, so they are fixed once the broach is made.
Tooth spacing is also a research topic. Iklodi, Munoa and Dombovari modeled chatter in broaching with a one-degree-of-freedom model and extended variable-pitch tuning formulas from milling to broaching tools. They checked the optimized tooth distances with time-domain simulations. That is a model result, not a shop trial. Treat it as a reason to ask the tool supplier about tooth distribution when chatter keeps returning on a given part, not as a setting you can change at the machine.
Checks, in order.
- Divide the length of cut by the tooth pitch. If the result is below two, a short part is riding on too few teeth. Ask the tool supplier whether a finer pitch is available, or whether parts can be held in a stack to lengthen the cut.
- Inspect clamping and tool mounting. A loose holder, an unsupported rear end on a long broach or a fixture that lets the part move can all let the edge shift relative to the work. For the holder's role in the load path, see what a broach holder is.
- Check slideway friction, covered below under ram motion. FUCHS links chatter marks at high surface pressure and slow feeds to an insufficient lubricating film on slideways.
- Only then change speed. Our guide to broaching speed and feed covers how speed, load and finish interact.
If chatter appears on one part number only and the tooth count is already two or more, the tool's tooth distribution and the part's stiffness are the next suspects. Record both before calling the supplier.
Torn, rough or burred surfaces: edge condition and cutting fluid
Symptom. Tears or galling streaks along the cut direction, a matte finish where a sheared-bright one is expected, or burrs at the entry and exit faces.
Surface defects have two main inputs you can inspect: the cutting edge and the fluid. Martinovic and Peterka tested the second one directly. They broached 24 internal grooves in C45 steel on a hydraulic broaching machine and measured roughness with a Mahr profilometer. The drawing required Rz 25 µm. With a cutting oil, the grooves measured Ra 0.509 µm and Rz 4.141 µm. With a 15% emulsion, they measured Ra 0.771 µm and Rz 8.731 µm. The authors report the oil result as 34% better in Ra and 53% better in Rz, and both fluids met the Rz 25 µm requirement.
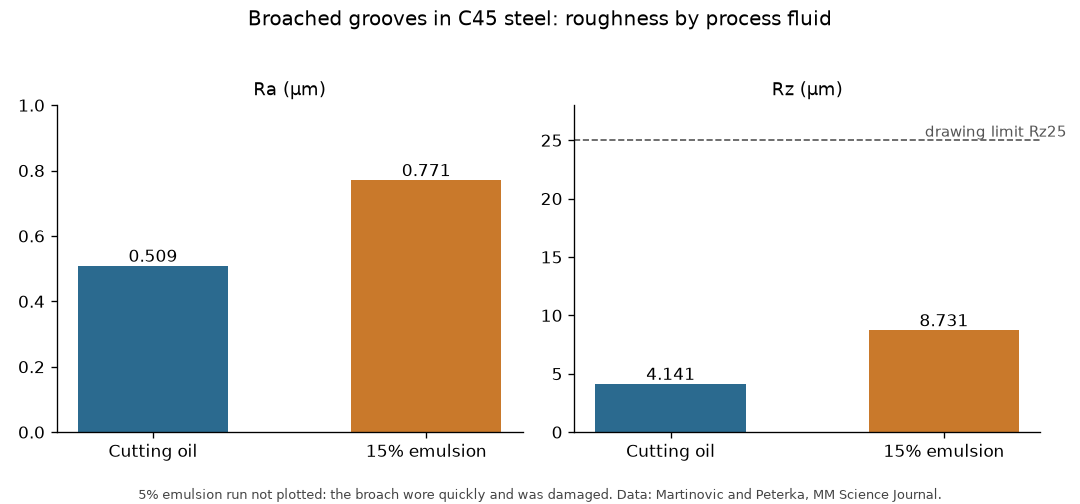
The 5% emulsion run behaved differently. The authors report that the broach wore quickly and was almost damaged, so no roughness value exists for it. They concluded that the emulsion concentration mattered for the process. The result is for one machine, one steel and one tool. It does not give a concentration to copy. It does show that a fluid that is too lean can end a tool's life, so concentration is a first check when wear and finish change together.
Master Fluid Solutions states the same principle for water-miscible fluids in general. Every such fluid is designed to run within a specific concentration range, and running below it frequently brings corrosion, tool-life and sump-life problems. Its technical bulletin also warns that a refractometer tends to read higher than the actual concentration as tramp oil enters the fluid, and that in a heavily contaminated system a clear reading is often not possible. The same bulletin describes alkaline titration and the acid split as other checks.
Checks, in order.
- Look at the edge. Adhesion, rounding or chipping on the teeth point to a regrind. Our guide to when to resharpen a broach tool and the broach reconditioning guide cover the regrind decision.
- Check the fluid against the supplier's design range, using a method that suits the fluid. If the sump carries tramp oil, confirm the refractometer reading by titration or an acid split.
- Confirm the stream reaches the cutting zone. A clear nozzle aimed at the tool shank cools nothing at the teeth.
- For burrs, compare the current work-material lot with the lot that ran clean: composition, hardness and structure. Quarantine mixed lots until checked.
- If finish stays rough on a freshly reground tool, have the finishing teeth checked against the tool drawing.
Our article on choosing a cutting fluid for broaching machines covers fluid selection.
Out-of-tolerance features and gauge failures: tool, machine or process
Symptom. Keyway width, spline profile or bore size drifts out of tolerance. The go-gauge binds or the no-go gauge passes.
Do not decide between tool, machine and process by feel. Martinovic and Peterka show a practical test. They measured the hole diameter on 50 impeller hubs, with a tolerance of 48 h10 (−0.1 mm), and computed the machine capability indices Cm and Cmk. Cm describes how many times the spread fits into the tolerance width. Cmk is the same figure corrected for position. They report Cm of 2.58 and Cmk of 2.01 against a required 1.67, and read this as a machine in good condition and well centered.
The difference between the two indices is the useful part. A high Cm with a low Cmk means the spread is small but the process sits off-center in the tolerance band. That points to setup, datum or tool size. Low values on both mean the spread itself is too large, which points to wear, looseness or variation in the incoming material. If Cmk equals Cm, the process is centered.
Checks, in order.
- Measure a sample of consecutive parts and calculate Cm and Cmk, using the same gauge for all of them. A sample of 50 is the size used in the study above.
- Gauge the feature at entry, middle and exit of the cut. Taper along the cut suggests progressive tooth wear or machine geometry. A uniform error suggests tool size or elastic recovery of the part.
- Measure a finished part unclamped. Distortion that disappears when released points to the fixture.
- Check the starting hole. A pilot hole that is off-center or out of round hands its error to the broached feature.
- Compare the broach's remaining regrind stock with the drawing. Our guide to broach tool life explains how regrinds change the tool.
If the go-gauge binds while the no-go gauge also fails, look for burrs at the entry face before suspecting size. A burr can hold a gauge out while the feature is within tolerance.
Stalls, chip packing and broken teeth
Symptom. The ram slows and stops mid-stroke, or a tooth tip is found chipped or a broach is snapped after a pull.
Chip space is the first thing to check. Schneider's handbook chapter explains that gullet depth depends on the tooth rise, the pitch and the workpiece material. The root radius is usually shaped so that chips curl tightly and take little room. It also describes chipbreakers: notches ground into roughing and semi-finishing teeth to prevent chip packing and help chip removal. They are vital on round broaches. Without them, the tool would cut ring-shaped chips that wedge into the gullets and eventually break the tool.
Two other items in the same chapter matter for breakage. A push broach is a column in compression, so it has to be short, and it will buckle and break under too heavy a load. When broaching slots, the sides of the teeth rub the sides of the slot unless side relief is provided, which causes rapid tool wear.
Checks, in order.
- After the stroke, clear and inspect every gullet. Packed chips or welded chips mean the stroke ran out of chip space.
- Check that the broach's chipbreaker pattern is intact on round tools. If a regrind has removed or blunted the notches, chips may form rings again.
- Compare the length of cut and stock removal with what the broach was designed for. Ask the supplier for the design range if you do not have it. If the cut exceeds the design range, shorten the cut or change the tool rather than forcing it through.
- On push broaching, check the tool's length against its diameter. Our article on how to avoid broach breakage covers installation and alignment.
- Confirm the pull capacity of the machine against the load. Stalling with a healthy tool and clean gullets means the cut needs more force than the machine delivers.
A stall with rising motor or pressure load usually comes before breakage. Treat a stall as a warning and inspect the tool before the next stroke.
Uneven ram motion and slideway friction
Symptom. The ram or sliding seat hesitates, crawls or moves unevenly. Sometimes the only sign is a degraded finish on the workpiece.
FUCHS, a lubricant manufacturer, describes the mechanism. Stick-slip is a frictional vibration caused by constantly changing friction between a slide and its slideway, because the roughness peaks on the two surfaces key into each other and must ride over each other. The company states that the dimensional accuracy and surface finish of machined parts are strongly influenced by stick-slip behavior of slideways and guide rails. A lubricating film with enough adhesion must be present to avoid chatter marks at high surface pressure and slow feeds.
Schneider's chapter adds a design comparison. Electromechanically driven horizontal surface machines are replacing older hydraulic ones for some applications because of their smooth ram motion and the resulting improvements in surface finish and part tolerances. The point for troubleshooting is that ram motion quality is a measurable machine property and that it affects the part.
Checks, in order.
- Confirm that the lubrication system is delivering oil to every slide surface: pump running, lines clear, reservoir at level.
- Check that the oil in the slideway system is the oil the machine builder specifies. FUCHS notes that slideway oils carry anti-stick-slip additives, and that hydraulic oils and slideway oils must be compatible when circuits are combined.
- Look at the guide rails for wear or scoring, and measure straightness if the finish pattern follows the stroke.
- Rule out hydraulic causes in the next section before calling the guides worn.
Hydraulic pressure loss, noise and aeration
Symptom. Falling or fluctuating pull force, ram drift, oil at fittings, a knocking or rattling pump, or heat in the hydraulic unit.
Ram force is cylinder pressure multiplied by piston area, so any pressure loss cuts the force available to the broach directly. The most useful published guidance concerns the reservoir and the pump inlet. Holdmeyer, writing in Tribology & Lubrication Technology, gives a rule of thumb for industrial applications: a reservoir sized at three times the system's total pumping capacity gives the fluid about three minutes of residence time to cool, release entrained air, drop out water and settle particles.
The same article explains how air gets in. Return piping should end below the fluid level. If the level drops below the end of the return line, air is beaten into the oil and causes foam and entrainment that may not clear. A low level can also let a vortex form at the pump inlet, drawing air in. Air that reaches the pump inlet is likely to cause aeration and erosion damage.
Cavitation has a different cause. If inlet piping has several elbows, is dented, or is smaller than the inlet port, the pressure at the pump inlet can drop enough for dissolved air to come out of solution. A plugged intake screen does the same. Holdmeyer says a sound like marbles or gravel flowing through the pump points to the inlet piping or the screen.
Checks, in order.
- Check the oil level at the sight gauge with the ram retracted, and look for foam in the reservoir.
- Confirm the return line ends below the fluid surface.
- Inspect the inlet piping for dents, extra elbows and loose joints, and clean the intake screen.
- Check for external leaks at fittings, hoses and seals. Fix leaks parts-first rather than topping up the reservoir.
- Only if the checks above are clean, test pump delivery and relief-valve setting against the machine builder's specification. Our article on the common failures of hydraulic broaching machines covers the fault catalog in more detail.
Our preventive maintenance checklist puts the level, filter and leak checks on a fixed routine.
Frequently Asked Questions
What causes chatter in a broaching operation?
Too few teeth in the cut, weak clamping or mounting, and slideway friction are the checks to run first. The chatter section above gives the order, and the tooth-engagement rule comes from Schneider's handbook chapter.
Why does a broach break?
The published mechanisms are chip packing, push-broach buckling and side rub in slots. Clear the gullets after each stroke and check the length of cut against the tool design, as described under stalls and breakage.
How do I tell a tool problem from a machine problem?
Measure a sample and compare Cm with Cmk, then gauge entry, middle and exit. The tolerance section above explains how to read the results.
Can I switch from cutting oil to an emulsion?
One published test did it on a C45 workpiece, but it needed 15% and the roughness was worse than with oil. Run your own trial with the broach, the steel and the fluid you plan to use, and monitor tool wear from the first stroke.
Send us the failure details
If a failure on this list has your line stopped, send us the part drawing, material, broach description and a photo or measurement of the defect. We will tell you whether the next step is a setup change, a tool conversation or a machine-side check. Use the contact page and include the three facts from the first section: what it looks like, when it started and what changed last.
References
- Technology of Broaching – Research of the Roughness and Machine Capability — Martinovic and Peterka, MM Science Journal: roughness by process fluid and capability indices.
- Analytical and numerical optimization of broaching tool tooth distribution — Iklodi et al., Meccanica: tooth distribution and chatter stability.
- Chapter 14: Broaches and Broaching — Schneider, Cutting Tool Applications: pitch, chipbreakers and push broaches.
- Concentration Control of Coolants — Master Fluid Solutions Technical Bulletin 032: concentration range and refractometer reading.
- Fundamentals of hydraulics: Reservoir designed to do more than hold the fluid — Holdmeyer, Tribology & Lubrication Technology: reservoir sizing, aeration and cavitation.
- Slideway Oils — FUCHS brochure: stick-slip and slideway lubricating film.