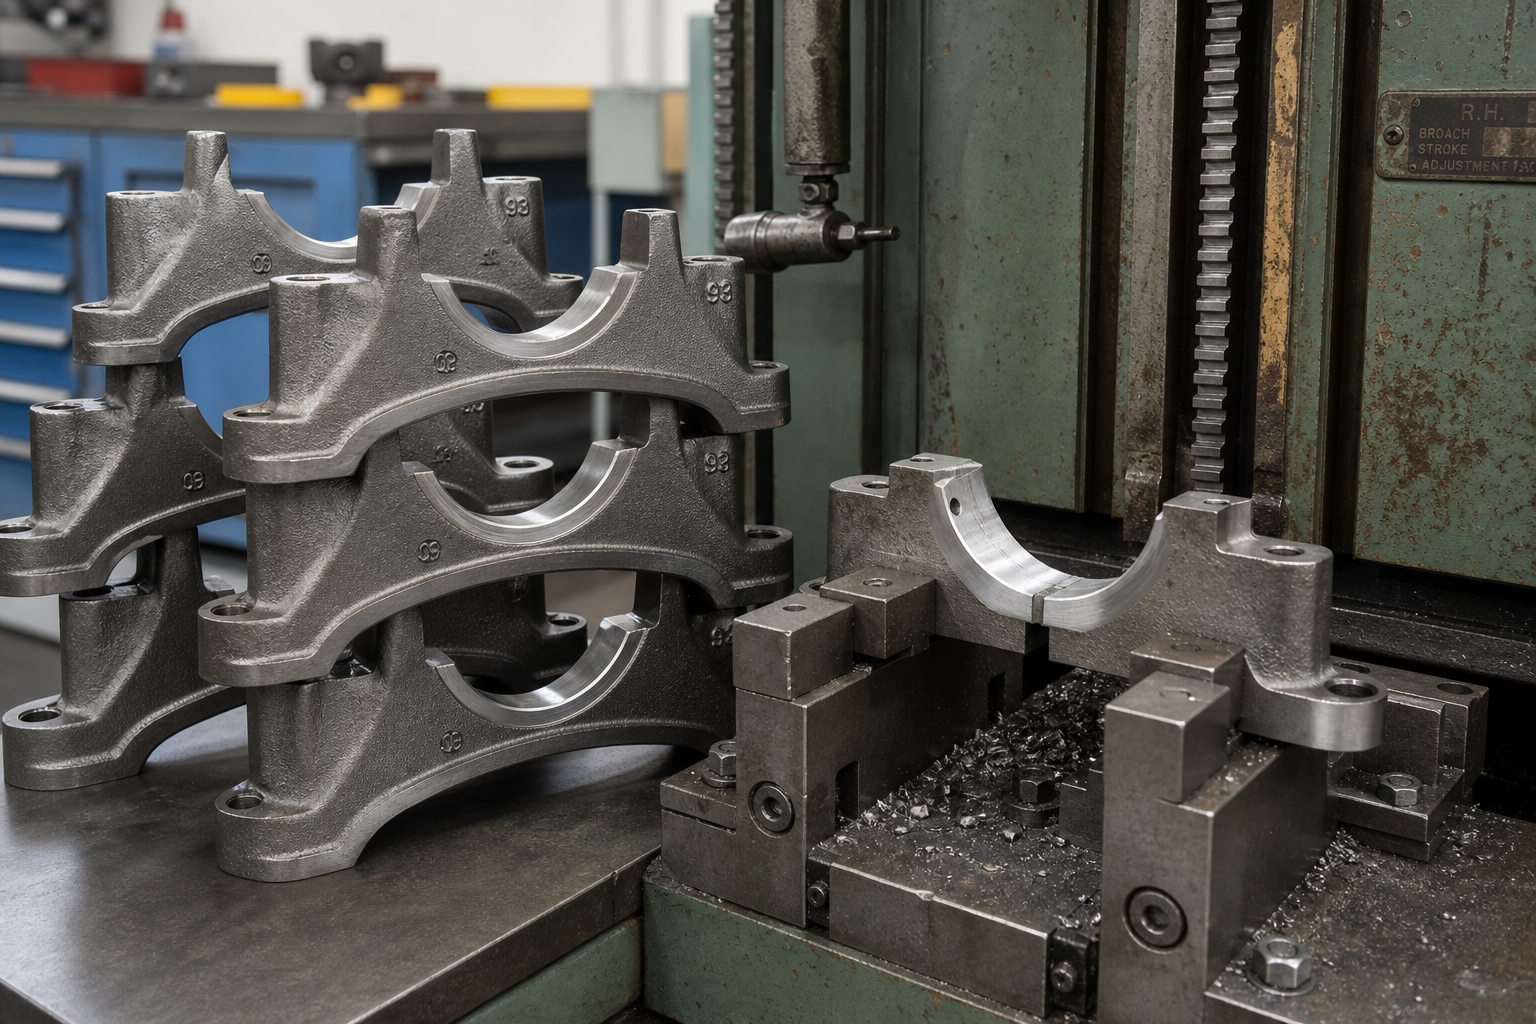
Cutting fluid selection for broaching starts with the workpiece, the broach and the way fluid reaches the teeth. A useful choice must provide lubrication under the actual cutting load, move chips away, work with the machine and meet the shop's handling requirements. Straight oil and water-miscible fluids are both used for broaching; the right formulation and delivery method depend on the job.
Table of Contents
- How Cutting Fluid Works in Broaching
- Compare Cutting Fluid Types
- Match the Fluid to the Broaching Job
- Deliver Fluid Where the Tool Cuts
- Evaluate Cutting Fluid with a Controlled Trial
- Maintain Fluid and Control Exposure
- Cutting Fluid Questions
- Choose the Next Step
How Cutting Fluid Works in Broaching
A broach removes material with successive teeth. Each tooth needs a clear path for the chip and a stable contact condition at the cutting edge. Fluid can lubricate the tool–chip interface, carry heat away, help remove chips and protect exposed metal surfaces. The relative importance of each function changes with the material, tool geometry and process conditions.
The National Institute for Occupational Safety and Health (NIOSH) describes metalworking fluids as a group that includes straight oils and water-miscible formulations. Its metalworking fluids resource discusses reducing heat and friction and removing metal particles. A product's name alone does not establish how well it will perform in a particular broaching operation: the complete formulation and how it is applied matter.
For an internal feature, watch whether chips leave the bore and whether the fluid reaches the active teeth. For a surface feature, examine how the stream meets the cutting zone and where chips collect. In either case, compare the fluid against the part's dimensional and surface requirements, the tool supplier's limits and the machine's delivery system.
Lubrication and heat removal serve different needs
Lubrication helps manage friction and adhesion at contacting surfaces. Heat removal depends on both the fluid and the way it is delivered. A shop should not select a fluid by assuming that every low-speed operation needs the same viscosity or that a water-based product is automatically suitable for every tool and workpiece.
Ask the supplier for the product's intended operation, workpiece materials and compatibility information. Review the safety data sheet and technical data sheet together. If the material, coating or machine seals are outside the listed applications, obtain a written compatibility assessment before a production trial.
Compare Cutting Fluid Types
NIOSH groups metalworking fluids into straight oils, soluble oils, semi-synthetics and synthetics. Straight oils are used without deliberate dilution with water, while soluble-oil concentrates form emulsions when mixed with water. Semi-synthetic and synthetic products have different compositions; consult the actual formulation rather than assigning every product the same properties.
| Fluid family | Practical selection question | Operating consideration |
|---|---|---|
| Straight cutting oil | Does the application need the product's specified lubricating and antiweld characteristics? | Check delivery, cleaning, fire precautions and compatibility with downstream washing. |
| Water-miscible fluid | Does the supplier approve the formulation for the material and broaching duty? | Mix and maintain the specified concentration; monitor water quality and contamination. |
| Semi-synthetic or synthetic | Does this particular product suit the tool, workpiece and system? | Verify the supplier's limits and the intended balance of cooling, lubrication and maintenance. |
The lubricant supplier FUCHS lists both water-miscible products and neat oils for steel broaching. That establishes that more than one fluid route is available, not that the products are interchangeable on every machine. Compare the relevant data sheets and carry out a controlled job-specific trial before changing a qualified process.
Check material and additive compatibility
The workpiece alloy is the starting point, but its processing condition also matters. Share the material designation, heat treatment and feature geometry with the fluid and tool suppliers. Ask whether the formulation is compatible with the workpiece, the broach material and coating, as well as machine components exposed to the fluid.
Avoid broad rules such as excluding every oil from every copper-containing alloy. Additive chemistry differs by product. Obtain the supplier's compatibility guidance for the actual alloy, contact time and cleaning process, and inspect trial parts for staining or corrosion. The same discipline applies when changing from a ferrous workpiece to an aluminium alloy or moving between suppliers.
Match the Fluid to the Broaching Job
Define the operation before comparing products. Record whether the feature is internal or external, the tool construction, the workpiece condition, the surface requirement and the part-cleaning route. Give the suppliers the same information so their recommendations address the same problem.
For a difficult internal profile, chip space and access to the cutting zone deserve particular attention. A fluid that appears suitable in a sample container still needs a delivery path that reaches the teeth during the stroke. For a surface operation, inspect the stream position along the working length and the route chips take out of the fixture.
Read the process signals together
A rising load, a rough surface or chips sticking to the teeth is a reason to investigate, not proof that fluid alone is responsible. Tool wear, stock condition, alignment, clamping and delivery can also change the result. Document the symptoms before adjusting several variables at once.
Use the broaching troubleshooting guide to organize a check of tooling and setup. If the broach shows wear, consult the tool resharpening guide and the tool supplier before continuing the trial. Comparing a new fluid against a worn tool can obscure the result and put the part at risk.
Do not transfer a concentration from another process
The fluid supplier's recommended range is the starting point for a water-miscible product. OSHA explains that both low and high concentrations can cause problems, including reduced protection or excessive residue and skin irritation. Make concentration an observed variable during the trial, not a number copied from a different machine.
A paper in MM Science Journal tested an internal shaped surface with a particular emulsion at 5% and 15%. The authors reported rapid tool wear at the lower concentration and acceptable results in their higher-concentration test. Those figures describe that experiment; they are not a recommended mix for another fluid or broach. Follow the supplier's range and assess the result on the actual job.
Deliver Fluid Where the Tool Cuts
The delivery path is part of the selection. Locate the nozzle or feed passage so that the relevant teeth receive fluid throughout the stroke. Check flow at the working position with the machine safely stopped and follow its operating instructions when checking the running condition. A blocked filter or a misdirected nozzle can make an otherwise suitable fluid ineffective.
OSHA recommends designing metalworking-fluid delivery to limit mist and describes the value of adequate flow directed to the cutting zone. Enclosure, collection and maintenance must suit the actual system. More pressure is not automatically better: OSHA notes that high-pressure delivery can generate mist and still fail to provide adequate fluid or chip removal in some circumstances.
Internal features and trapped liquid
Internal geometry can restrict both chip evacuation and fluid escape. Make room for the tool, chips and fluid in the setup, and follow the tool supplier's application instructions. Blind features demand a specific review of the available exit path rather than an assumption that fluid can escape freely.
Slater Tools advises applying fluid to the tool tip rather than filling the pilot hole for its internal rotary broaching in blind holes, because trapped fluid can prevent full depth. This guidance is specific to that rotary process and tool system. For a different broach or machine, obtain the relevant supplier's instructions instead of transferring the procedure unchanged.
Dry and minimum-quantity routes
A dry trial and minimum-quantity lubrication are distinct operating choices. The latter applies a controlled amount of lubricant; neither route should be adopted merely because the fluid tank can be turned off. Evaluate the tool, workpiece, chip evacuation, guarding and extraction requirements with the machine and tool suppliers.
Research published in Friction examined a soybean-oil formulation with nanographite in a broaching study using minimum-quantity lubrication. The experimental formulation and equipment are part of the result. It is a research route to investigate with qualified suppliers, not an instruction to add particles to a production sump.
Evaluate Cutting Fluid with a Controlled Trial
Start with an approved process baseline. Record the workpiece specification, tool condition, setup, speed, fluid identity and delivery arrangement. Define the part acceptance criteria, inspection method, stop conditions and personnel responsible for the test. Where possible, keep the tool and setup comparable between the baseline and the candidate fluid.
| Observe | What to record | Why it matters |
|---|---|---|
| Part condition | Feature size, finish, burrs and visible staining | The fluid must fit the finished-part requirements and cleaning route. |
| Tool condition | Wear, adhesion, chipped edges and chip packing | A short run should not conceal a developing tool problem. |
| Machine signals | Load trend, fluid delivery and filter condition | Changes help identify whether the cutting zone is being supplied consistently. |
| Fluid condition | Product, mix where applicable, contamination and appearance | The test is only interpretable if the fluid state is known. |
Inspect the first parts and continue sampling at planned intervals. A successful first piece is useful, but it cannot by itself demonstrate performance over a representative production run. Stop if the agreed limits are exceeded, isolate affected parts and return to the validated route while the cause is investigated.
The MM Science Journal study also reported surface roughness for its tested internal groove: the oil condition produced Ra 0.509 µm, while the tested higher-concentration emulsion produced Ra 0.771 µm. These are measurements from that study, not expected results for another setup. They illustrate why a trial should measure the part as well as observe the tool.
Maintain Fluid and Control Exposure
A water-miscible product changes in service as water evaporates, fluid is carried out on parts and contaminants enter the sump. OSHA recommends checking concentration and maintaining it within the product's intended range. Use the fluid supplier's method and correction factor for the instrument, record readings and investigate repeated drift rather than adding concentrate by guesswork.
Check the makeup water against the supplier's requirements. OSHA notes that dissolved minerals can contribute to deposits and other fluid problems. Remove chips and unwanted oil using equipment appropriate to the system, and keep fluid return paths accessible for inspection. Follow the supplier's maintenance and cleaning instructions when changing products.
Protect people and the working environment
NIOSH and OSHA identify skin contact and inhalation of metalworking-fluid mist as exposure routes. Use suitable enclosure and ventilation, maintain the collection system, and establish work practices for handling contaminated parts and clothing. A safety data sheet is a starting point; the site's assessment must also consider the fluid in use and its contaminants.
Manage spent fluid, filters and contaminated absorbents under applicable local requirements and the waste contractor's instructions. Do not assume that a fluid is safe to discharge or dispose of solely because it is labelled vegetable-based or synthetic. Keep the product identity and service records available to the people responsible for disposal.
Cutting Fluid Questions
Can the same product be used for every workpiece?
Not without checking its specified material compatibility and the process. Different alloys, tool coatings, cleaning systems and corrosion requirements can call for different formulations. Ask the fluid supplier to review the full job rather than relying on a generic material label.
What should be checked when a fluid smells unusual?
Record the change and follow the site's fluid-management procedure. OSHA notes that an unpleasant odour can indicate uncontrolled microbial growth; concealing the smell does not address the cause. Ask the responsible fluid specialist to investigate, test and recommend corrective action.
Does a clear sump mean the cutting zone is receiving enough fluid?
No. Sump appearance does not establish nozzle position, flow at the teeth or filter condition. Check the delivery route using the machine's safe procedure and compare the observed supply with the tool and fluid suppliers' instructions.
Should a shop change fluid when a broach wears early?
Investigate the tool, stock, alignment, chip evacuation and delivery as well as the fluid. Record the evidence and change variables in a controlled way. The tool supplier can help determine whether resharpening or a setup correction is needed before a fluid comparison.
Choose the Next Step
The strongest cutting fluid choice is the one that has been checked against the actual broach, material, fluid delivery and part requirements. Shortlist products with supplier-supported compatibility, then compare them against the existing process using documented part and tool observations. If you are planning a new job or reviewing a delivery arrangement, contact our team with the material, feature and production requirements.
References
- Metalworking Fluids: Safety and Health Best Practices Manual — OSHA guidance on concentration, delivery, maintenance and exposure controls.
- Metalworking Fluids — NIOSH resource describing fluid classes, functions and health risks.
- Broaching — FUCHS examples of water-miscible and neat fluids for steel broaching.
- Fluids, Lubrication, Parts and Tool Care — Slater Tools guidance specific to rotary broaching.
- Technology of Broaching: Research of the Roughness and Machine Capability — MM Science Journal experiment on fluid concentration and measured surface roughness.
- Penetration and lubrication evaluation of vegetable oil with nanographite particles for broaching process — Friction research on an experimental minimum-quantity lubrication formulation.