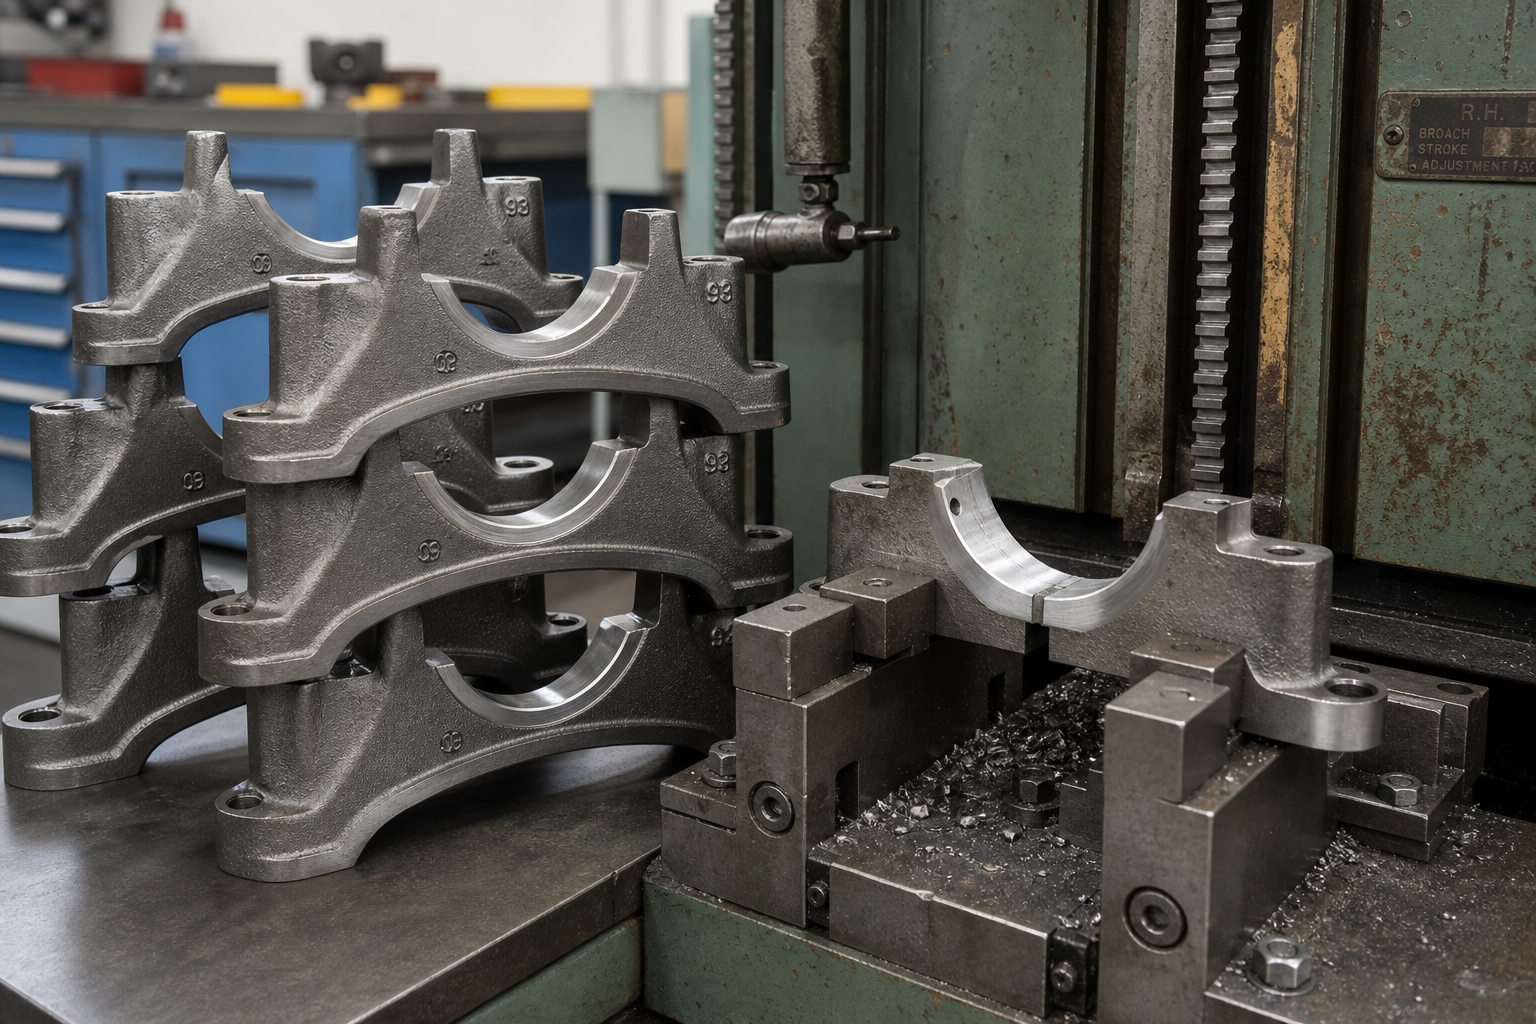
What is broaching, and why do high-volume plants keep choosing it over milling and shaping? Broaching is a production machining process that finishes an internal or external surface with a multi-toothed cutter called a broach, in a single stroke. Because the broach carries roughing, semi-finishing and finishing teeth in one tool, it replaces the many passes and tool changes of general-purpose machining with one guided pass — which is also why it earns its keep at production volumes rather than in one-off work.
This guide walks through the process itself, the main broaching methods, the common broach shapes, the machine classes that drive them, the materials they cut, the accuracy you can expect, and where broaching sits in real production.
Table of Contents
- What Is Broaching?
- How Does the Broaching Process Work?
- Linear vs. Rotary Broaching
- Pull and Push Broaching
- Internal and External Broaching
- Common Types of Broaches
- Types of Broaching Machines
- What Materials Can Be Broached?
- Broaching Accuracy and Surface Finish
- Common Broaching Applications
- Frequently Asked Questions
- Get Expert Help Choosing a Broaching Machine
- References
What Is Broaching?
Broaching is, in the definition of the machining handbook section by Kalpakjian, "a production process whereby a cutter, called a broach, is used to finish internal or external surfaces such as holes of circular, square, or irregular section, keyways, the teeth of internal gears, multiple spline holes, and flat surfaces." The cutter is a long, multi-toothed tool in which every tooth stands slightly taller or wider than the one before it, so each tooth removes a small, predictable chip and passes the remaining stock to its neighbor. Roughing, semi-finishing and finishing happen in the same stroke, on the same tool.
That single-stroke character is what separates broaching from processes that need many passes. A milled or shaped keyway takes a series of cuts with indexing between them; a broached keyway is complete when the broach exits the other side. The trade is tooling economics: a broach is an expensive, purpose-built tool, so the process pays best where volumes are high and the part repeat — keyways, splines, non-circular holes and flat or profiled surfaces, typically on small to medium castings, forgings and bar-stock components. To see the equipment that drives the tool, read our companion guide on what a broaching machine is.
How Does the Broaching Process Work?
Every broaching operation pairs the same elements: the broach itself, the workpiece, a fixture that holds the workpiece in line with the stroke, and cutting fluid. The cutting mechanics live in the tooth geometry.

The pitch — the distance from one tooth to the next — is set by tooth strength, chip size and the length of the cut. Kalpakjian gives the working formula for roughing teeth as p = 0.35 √(2l), where l is the length of the hole or surface being cut, and reports average pitches of 1/8 to 1/4 in (3.175 to 6.35 mm) for small broaches and 1/2 to 1 in (12.7 to 25.4 mm) for large ones. The same section insists that "at least two teeth should be in contact with the workpiece at all times"; on short surfaces, teeth are often cut on an angle or helix so that at least two cut simultaneously.
Each tooth rises by a small amount per tooth rather than by one deep pass. For medium-sized broaches the taper per tooth is 0.001 to 0.003 in (0.025 to 0.076 mm); large broaches remove 0.005 to 0.010 in (0.127 to 0.254 mm) per tooth or more. The feed for broaching cast iron is approximately double that for steel, because the material chips more freely. Teeth carry a front rake angle of 5 to 15° to curl the chip and cut clean, and the final teeth take progressively smaller increments, with the last few at nearly zero taper — or, for soft metals, plain rounded lands a trifle larger than the last cutting tooth that burnish instead of cut. Broaches are generally made of M2 or M7 high-speed steel, with carbide used for the teeth of large broaches.
Key takeaways
- Pitch follows the cut length: p = 0.35 √(2l), averaging 1/8–1/4 in on small broaches and 1/2–1 in on large ones, with at least two teeth always in contact.
- Stock removal is distributed: 0.001–0.003 in per tooth on medium broaches, up to 0.005–0.010 in on large ones, roughly double for cast iron versus steel.
- One tool carries M2/M7 high-speed-steel roughing, semi-finishing and finishing (or burnishing) teeth through the whole operation.
The stroke itself is over in seconds: the fixture locates the part, the machine drives the broach past or through it once, and inspection follows. For tool design and sizing in depth, see our complete guide to broaches.
Linear vs. Rotary Broaching
Linear broaching is the most common form: the broach moves in a straight line across or through the workpiece, and every tooth takes its slice as it passes. The diagram below shows the idea in three steps — the in-feed per tooth, the full broach with progressively rising teeth, and the finished cut with chips curling out of the gullets.

Rotary broaching — also called wobble broaching — takes a different route to a finished polygon. It runs on lathes, mills and machining centers rather than on a dedicated broaching machine, cutting hexagons, squares, serrations, involute splines, keyways and similar forms in one pass. The mechanism, in the words of tool maker Polygon Solutions, is that "the holder is offset 1 degree from the centerline of the shank allowing the broach to enter the part at an angle, only cutting one portion of the form at a time." The part needs a pilot hole slightly larger than the form's minor diameter and slightly deeper than the broached depth, plus a chamfer slightly larger than the major diameter. Typical rotary practice runs 500–700 RPM at 0.001–0.003 in per revolution; the practical limits are a broached depth of about 1.75 in and major diameters up to about 2 in.
For the full treatment of the wobble process, read what is rotary broaching, and for choosing between the two, see rotary broaching vs. conventional broaching.
Pull and Push Broaching
Pull Broaching
Pull broaching draws the broach through the workpiece, and it is the workhorse for internal work. A pull broach is long and carries many teeth; the tension of pulling works in the tool's favor. As Kalpakjian puts it, "pulling tends to straighten the hole, whereas pushing permits the broaches to follow any irregularity of the leader hole." The tool below shows the anatomy: a pull end that engages the machine's pulling mechanism, a neck, a front pilot that enters the pre-drilled hole, the toothed body, and a rear pilot. At the machine, the pull end attaches by a key slot and key, a threaded connection, or a head that fits an automatic broach puller.

Push Broaching
Push broaching drives a shorter, stiffer tool through the part, usually on press-type machines. Push broaches "are usually shorter than pull broaches, being 6 to 14 in (150 to 350 mm) long, depending on their diameter and the amount of metal to be removed," Kalpakjian notes, and they usually have a large cross-sectional area to stay rigid under compression. Where accuracy demands it, four to six push broaches of increasing size run in sequence as a set, each taking part of the stock.
The choice is a part-geometry decision, and our push broaching vs. pull broaching comparison walks through it side by side.
Internal and External Broaching
Internal broaching finishes the inside of a hole. The part must first carry a prepared leader hole — drilled, reamed or cored — because the broach only removes stock from that pilot onward; this makes internal broaching a finishing operation, not a roughing one. Round, hexagonal, spline and keyway holes are the classic cases. A special case is blind broaching, where the tool does not pass through the part: it stops partway and leaves a blind cavity, as with the internal splines below.

External (surface) broaching cuts the outside of the part — flats, steps and profiled forms such as serrations and keyways on outside diameters. The same progressive-tooth logic applies; only the direction of engagement changes. Where a form is deeper than one broach can carry, the stock can be split across several passes; our multi-pass broaching guide covers that practice.
Common Types of Broaches
Broaches are shaped by the form they cut. The reference chart below pairs each internal hole profile with the broach that produces it: square, round, single and double keyway, 4-spline, hexagon, rectangular, double-cut, internal gear and helical groove.

A few families cover most production work. Keyway broaches are flat bars with teeth along one surface, cutting the slot that locks a gear or pulley to a shaft — the slot usually guided by a slotted bushing in the hole; our keyway broaching guide covers them in depth. Spline broaches cut the ridges and grooves of splined holes that transmit torque in driveshafts and gearboxes; involute splines follow gear-tooth profiles, and the spline broaching guide treats the tooth forms. Round broaches size and finish circular holes in one pass. Surface (slab) broaches cut flats and profiled outside surfaces. Beyond these, special broaches are built for hexagons, dovetails and other custom sections to print.
Types of Broaching Machines
The machine's job is simple to state and demanding to do: drive the broach or the workpiece through one accurate stroke while holding the part rigidly. Kalpakjian summarizes the two families: push broaching runs on machines "of the press type" — usually vertical, and driven hydraulically or by screw, rack or crank — while "the pull type of broach may be either vertical or horizontal," with the ram again driven hydraulically or by screw, rack, or crank.
In practice the classes sort by part and stroke. Horizontal machines suit long internal pulls and large parts, at the cost of floor space; vertical machines save floor space and dominate surface-broaching work; surface broaching machines carry the tool along a guided track for outside cuts. Modern lines add servo and CNC control for positioning, stroke profiles and hard-material cuts. We cover each class in detail: the horizontal broaching machine guide, the vertical broaching machine guide, and the head-to-head difference between horizontal and vertical broaching machines; for outside work, the surface broaching machine guide, and for motion control, the CNC broaching machine guide.
What Materials Can Be Broached?
Most machinable metals take broaching well; what changes is the speed. Kalpakjian's data puts cutting speeds "from 5 ft/min (1.5 m/min) for high-strength materials to as high as 30 to 50 ft/min (9 to 15 m/min) for aluminum and magnesium alloys," with M2 and M7 high-speed steels and carbides as the tool materials. Cast iron machines freely — its permissible feed per tooth runs about double that of steel.
Cutting fluid is part of the process, not an afterthought. Oil-in-water emulsions are the general-purpose choice; Kalpakjian notes that the more concentrated 1:10 mixtures are used for broaching, threading and gear cutting, while broaching of refractory and high-temperature alloys requires highly compounded oils.
Rotary broaching extends the same material range with the right tool steel. Polygon Solutions lists aluminum, brass and mild steels as ideal, and reports that powdered-metal tool steels such as PM M-4 and PM T-15 make rotary broaching "successful in materials such as titanium, 300 and 400 series stainless steel and Inconel." On hardness, our own application guidance is that tool life is good below HRC 25, decreases markedly above it, and that broaching is not recommended above HRC 32 — see our FAQs. The material-by-material breakdown, including cutter recommendations, is in what materials can be broached.
Broaching Accuracy and Surface Finish
For round holes, broaching sits above reaming on both counts. Kalpakjian states it directly: "Broaching round holes gives greater accuracy and better finish than reaming." The finishing teeth of the broach take near-zero increments and can burnish, so the final surface is generated by the last few teeth rather than by a separate finishing pass.
There is one caveat worth knowing before you sequence operations. Because the broach "may be guided only by the workpiece it is cutting, the hole may not be accurate with respect to previously machined surfaces" — so where the hole must hold a tight relationship to other features, Kalpakjian recommends broaching first and then turning the other surfaces with the workpiece mounted on a mandrel. Position the process in the routing, in other words, before you blame the broach for an alignment problem.
Common Broaching Applications
The features broaching finishes — keyways, spline holes and the teeth of internal gears — are exactly the torque-transmitting features of gearboxes, driveshafts and hubs, which is why engine and transmission plants run broaching at high volume. Diff housings, gear bores, coupling hubs and pump rotors all carry broached keys and splines.
The other classic home of the process is the turbine. Blade roots are mounted by their root in the turbine disk, and that root "is often designed as a 'fir tree profile' because of the high centrifugal forces," as metrology firm Mahr describes; the mating slots in the wheel are profiled broach slots. US Patent 8,079,817, which covers firtree and broach slot forms for a gas-turbine stage, describes the arrangement: "the third stage of a typical gas turbine can have as many as 92 buckets that radially extend from a rotor or wheel," each fitted into a corresponding broach slot. Fir-tree forms, serrations and involute profiles are standard territory for special-purpose broaches.
Beyond drivelines and turbines, broaching serves agricultural equipment, defense and general precision-mechanical parts wherever a profiled internal or external form repeats at volume. Where the geometry or batch size argues for another process, our comparisons — broaching vs. hobbing for gears and splines, and broaching vs. milling for internal keyways and profiles — set out the decision points.
Frequently Asked Questions
Should I choose push or pull broaching?
Let the part decide. Pull broaching suits long internal cuts and many teeth, and pulling tends to straighten the hole; push broaching uses shorter, stiffer tools of 6 to 14 in, often run as a set of four to six, and follows the leader hole rather than correcting it. The comparison section above works through the trade-offs.
Can broaching correct a hole that is out of position?
Only partially, and only in the pull direction. A broach is guided by the hole it is cutting, so a pulled broach can straighten the hole itself, but it will not reliably align the hole to previously machined surfaces. Where alignment matters, broach first, then finish the other features with the part on a mandrel.
Can I broach a hexagon on my existing lathe or machining center?
Yes — that is exactly what rotary broaching is for. With the 1°-offset holder, forms up to about 2 in across and about 1.75 in deep can be cut in one pass on lathes, mills and machining centers, in materials from aluminum and mild steel to titanium and Inconel with the right tool steel.
Get Expert Help Choosing a Broaching Machine
Broaching rewards a clear part brief: the feature to be cut, the material and its hardness, the volumes, and the tolerance the drawing actually demands. Start with our guide on how to choose the right broaching machine and the broaching machine price guide for budget planning — then contact our engineering team with your part drawing, and we will recommend a machine configuration and broach design for the job.
References
- Machining Processes and Machine Tools, Sec. 13.4 (by Serope Kalpakjian) — Kalpakjian; production definition of broaching, tooth pitch formula and values, taper per tooth, tool materials, push vs. pull broach lengths and behavior, machine types and ram drives, cutting speeds and cutting fluids, round-hole accuracy vs. reaming.
- Rotary Broaching FAQs — Polygon Solutions; the 1-degree holder offset, rotary-broachable forms, material range with PM M-4/PM T-15 tool steels, depth and diameter limits, and typical speeds and feeds.
- Turbine blade: "fir tree" inspection — Mahr Group; fir-tree profiles on turbine blade roots and the centrifugal loads behind them.
- Advanced firtree and broach slot forms for turbine stage 3 buckets and rotor wheels, US Patent 8,079,817 B2 — US Patent 8,079,817; broach slots in turbine rotor wheels, the 92-bucket third stage, and fir-tree bucket roots fitted into broach slots.