A horizontal broaching machine drives its broach along a level bed parallel to the floor; a vertical broaching machine drives it up or down an upright column. The difference between horizontal and vertical broaching machine layouts sounds small, but it drives everything worth comparing: stroke length, floor space, chip removal, part handling, automation, and cost. This guide walks through those seven factors and ends with a four-question framework for choosing.
Table of Contents
- What Is a Horizontal Broaching Machine?
- What Is a Vertical Broaching Machine?
- The Difference Between Horizontal and Vertical Broaching Machine Layouts
- How to Choose: A Four-Question Decision Framework
- Where Common Parts Usually Land
- Frequently Asked Questions
- The Bottom Line
- References
Every internal broaching project starts at the same fork in the road: should the ram drive the broach horizontally along a floor bed, or vertically down an upright column? Both layouts cut the same forms — keyways, splines, hexagons, flats, and contours — by pushing or pulling a multi-tooth broach through or across the workpiece in one linear stroke. The cutting physics do not change with orientation. What changes is everything around the cut: how much floor the machine occupies, how long a stroke it can deliver, how chips leave the work zone, how parts load and unload, and how the machine fits a production line.
This guide explains the difference between horizontal and vertical broaching machine configurations in seven factors that actually drive the buying decision, then closes with a four-question framework you can apply to your own parts. For the full treatment of either configuration, see our companion vertical broaching machine complete guide and horizontal broaching machine guide. New to the process itself? Start with our primer on what broaching is.
What Is a Horizontal Broaching Machine?
A horizontal broaching machine carries its ram on a level bed that runs parallel to the shop floor. The workpiece is fixtured stationary at working height, and the ram — guided on precision ways along the bed — pulls or pushes the broach through the part in one horizontal pass. Because the bed extends outward along the floor rather than upward, stroke capability grows with bed length instead of with building height.
Two structural facts define the category. First, the work zone stays open at both ends of the bed and from above, so heavy parts reach the fixture with the cranes, hoists, and roller conveyors that most shops already own. Second, most horizontal internal machines are pull-type: the ram drags the broach through the bore in tension, and a broach in tension cannot buckle. The same bed-and-ram architecture also serves surface broaching and continuous chain broaching, where fixtured parts ride past stationary broaches without stopping. For the basics, see what horizontal broaching is.
What Is a Vertical Broaching Machine?
A vertical broaching machine stands the stroke upright: the ram travels down or up a column, so the machine grows toward the ceiling instead of across the floor. The patent literature describes the architecture precisely. In Forst Technologie's 1998 patent US5833411A, the machine is built around "a machine stand having an upper rail and a lifting carriage displaceably guided on the stand and drivable by means of lifting spindles," with the workpiece holder mounted on the rail, in the patent's words "holding a broach when a compressive broaching job is carried out." Internal work dominates: keyways, splines, hex sockets, and polygon bores in gears, hubs, and fittings.
The variants differ mainly in which direction the slide works. In the pull-up arrangement of US3960056A, the machine "includes a workpiece holder mounted on a machining table," while "a vertically displaceable broaching slide is mounted beneath the machining table" and "draws a broach through a workpiece" upward. In the push-type arrangement of US6409442B1, the machine column carries "a workpiece lifting table which is guided for displacement on carriage guideways," with a feeder carriage underneath that pushes the broach up through the part. Typical work spans internal splines and keyways in transmission gears, hexagon sockets in fittings and hand tools, and bore forms in wheel hubs — parts that sit stably on a fixture table. For the basics, see what vertical broaching is.
The Difference Between Horizontal and Vertical Broaching Machine Layouts
The table below summarizes the seven factors; the sections after it explain the engineering reason behind each difference, because the "why" is usually what settles the argument on a specific part.
| Factor | Horizontal machine | Vertical machine |
|---|---|---|
| Stroke direction | Ram travels level along a floor bed | Ram travels up or down an upright column |
| Floor space and installation | Long, low footprint; standard slab, no pit | Compact footprint; stroke bounded by building height or pit depth |
| Stroke length ceiling | Grows with bed length; no practical ceiling | Long broaches get awkward to hang and support |
| Chip and coolant flow | Chips travel along the bed; flushing must be engineered | Gravity pulls chips and coolant down and out of the cut |
| Workpiece handling | Heavy parts load from above at working height | Parts load onto a fixture table; very heavy parts need lift planning |
| Automation pattern | In-line flow: conveyor in, cut, conveyor out | Overlapping cycles: indexing tables, shuttle systems |
| Cost profile | Generally lower purchase price; larger footprint | Higher entry price; saves floor and wins on cost per part at volume |
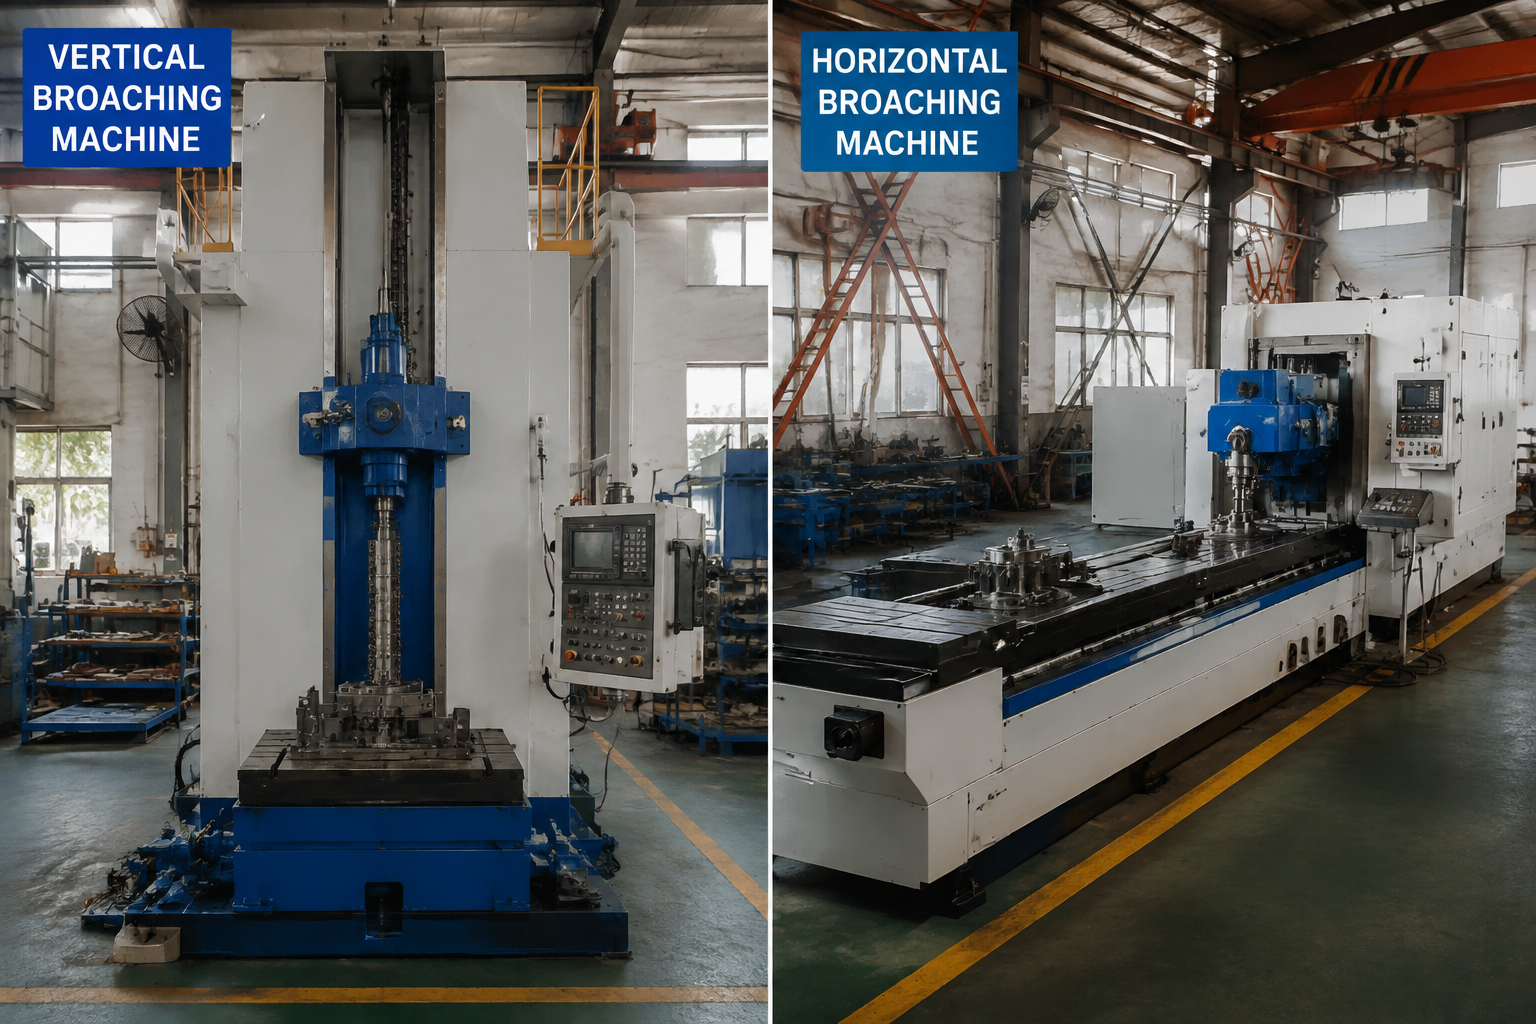
1. Stroke Direction and Machine Structure
The fundamental difference is geometric: a horizontal machine lays its stroke along the floor, a vertical machine stands it upright, and everything else follows. On a horizontal machine, the broach lies along its full length on the bed, supported and guided, and the part rests on level locators with the cutting force pressing it into its seat. On a vertical machine, the column carries the slide — as in US5833411A's lifting carriage on its upper rail — and the part sits on a table or fixture face directly in the tool path. Neither layout cuts better; they cut differently, and the part decides which geometry is convenient.
2. Floor Space and Installation
A horizontal machine trades height for length. The bed scales with stroke and broach length, so the machine occupies a long rectangle of floor — but it installs on a standard slab, needs no pit, and stays within ordinary ceiling height. A vertical machine makes the opposite trade: a compact footprint that fits inside a small cell, but a stroke bounded by the building. Some pull-down and table-up designs need overhead clearance or a floor pit to gain stroke, which means foundation work and a machine that is harder to relocate later. Low bays favor the horizontal layout; scarce floor space favors the vertical.
3. Stroke Length Capability
Why can horizontal machines run longer strokes? Because adding stroke on a floor bed means adding bed length, and there is no practical ceiling on that. A long internal spline or a deep keyway demands a long broach, and a long broach is a heavy, slender precision tool. Hung vertically, its own weight works against the guidance and support it needs; laid horizontally, the full length of the tool rests on the bed's support rollers and ways. Support matters beyond the day of purchase, too: rollers and guide shoes wear with stroke length and part weight, and a horizontal bed keeps that wear visible and serviceable at working height instead of overhead. This is why deep bores in tubes and barrels, and splines running the length of a shaft, are almost always cut horizontally. On a vertical machine, the stroke you can buy is the stroke your building can stand — plus pit depth, if you are willing to dig one.
4. Chip Removal and Coolant Handling
Vertical machines hold a structural advantage here, and the reason is gravity. As the broach cuts, chips and coolant fall away from the cutting zone and drain below, keeping finished teeth clear of debris and the part clean. On a horizontal machine, chips leave the cut at the same height they are created and travel along the bed, so the machine depends on engineered flushing, sloped beds, or chip conveyors to move them. The flushing has to be designed for the material as much as the machine: stringy chips from ductile steels need higher-volume coolant delivery and frequent conveyor cycles, while short-chipping cast irons tolerate a simpler system. Why does this matter enough to swing a decision? Recut chips trapped in the work zone score the finished surface and accelerate tooth wear, so difficult, stringy materials raise the premium on the vertical layout's natural cleanliness.
5. Workpiece Size, Shape, and Handling
Match the machine to the part's natural resting posture. Large, heavy, flat-backed workpieces — steering knuckles, control arms, cylinder blocks, large valve bodies — are awkward to stage upright but lie naturally on horizontal locators, and overhead cranes or rollers deliver them from the direction heavy parts prefer to move. Vertical machines favor parts that sit stable on a fixture table: gears, sprockets, hubs, pulleys, and disc-shaped components, exactly the workpiece-on-table arrangement the pull-up and push-type patents describe. Station height is part of the deal as well: a vertical table puts small parts at a comfortable working level for an operator with a chute or a feeder, while a horizontal fixture meets heavy parts at the height the crane delivers them. A general rule that holds well: if the part needs a crane, think horizontal; if it fits in two hands or a chute, vertical loading is faster and less fatiguing for the operator.
6. Automation and Line Integration
The two layouts automate in different patterns, and the pattern usually follows the plant's material flow. Horizontal machines suit in-line integration: parts arrive on a conveyor at fixed height, get broached, and leave in a straight line — the native rhythm of automotive transfer lines. Vertical machines suit overlapping cycles: rotary indexing tables and shuttle systems let one station load while another cuts, and pull-up machines place the loading station low, where bowl feeders and pick-and-place units want to work. Twin-slide vertical machines take this further, cutting two features or two parts in alternating strokes. Neither approach is inherently more productive; the question is which one matches the line the machine must join. See also our comparison of pull-up, pull-down, and push-type arrangements.
7. Machine Cost and Tooling Cost
Horizontal machines are generally the lower-ticket entry: the structure is simpler, the installation is a standard slab, and retooling between jobs is quick, which keeps tooling-related cost down when volumes are modest or part variety is high. Vertical machines — particularly servo-driven and twin-ram designs — carry a higher purchase price, but they repay it where floor space is expensive and volumes are high, because the compact footprint and faster automated cycles push cost per part down. One rule worth more than the price tags: if you already own a library of broaches from a horizontal machine, staying horizontal lets that inventory keep working. For a fuller breakdown, see our broaching machine price guide.
How to Choose: A Four-Question Decision Framework
Set the spec sheets aside for a moment and answer four questions about your own production. Each answer points at one layout, and when the answers disagree, weight them in this order.
Question 1: What does the workpiece look like?
Weigh the part and picture its resting posture. Long parts with features along their length, and heavy parts that arrive by crane, load and locate better lying flat — horizontal. Small and mid-size parts with internal features, and disc-shaped parts with large diameters, load faster onto a vertical fixture table — vertical. This first question eliminates more options than any spec comparison.
Question 2: How much stroke does the feature need?
Remember that stroke length is not the same as cut length: the ram must pull the entire broach clear of the work. Add the broach length, the part length, and clearances, then compare the total against your building's vertical budget. When the required stroke exceeds what your ceiling — plus any pit you are willing to excavate — can offer, the decision is made for you: horizontal.
Question 3: What does your floor space and building allow?
Measure the actual footprint available, not the one on the drawing. A long horizontal bed competes with aisles and adjacent cells; a tall vertical machine competes with cranes, mezzanines, and overhead utilities. Also check the foundation: a pit or special anchoring adds cost and permanence to a vertical installation, while a horizontal machine bolts to a standard slab and can move with the layout.
Question 4: How will parts load, unload, and flow?
Sketch the part's journey through the cell. If parts move on a conveyor line at fixed height — in-line flow — a horizontal machine accepts and releases them without a lift. If you want overlapping load-and-cut cycles, indexing tables, or feeder-fed small parts, the vertical layout is built for it. And if volumes are still uncertain, favor the machine that retools cheaply: that is usually the horizontal. For a deeper walk through this decision — tonnage, drive types, tolerance capability, new-versus-used — see our dedicated article on how to choose the right broaching machine.
Where Common Parts Usually Land
A shortcut built from shop-floor practice — useful for a first cut at the decision before the four questions are asked in earnest:
- Transmission gears, sprockets, pulleys, wheel hubs — internal splines and keyways in mid-size parts: vertical, usually pull-down or pull-up.
- Fittings, hex sockets, hand-tool components — small parts at high volume: vertical push or pull-up, feeder-fed.
- Steering knuckles, control arms, crossmembers — heavy castings with exterior surfaces: horizontal surface machines.
- Cylinder blocks and heads — large castings, multiple features: horizontal, in-line with the machining line.
- Long shafts, tubes, barrel bores — deep features along the length: horizontal internal machines; no practical vertical alternative.
- Lever forks, link ends, pads in very high volume — small external features: horizontal continuous chain machines.
Treat the list as a starting point, not a verdict — tolerances, materials, and volumes can move a part from one column to the other. When two of the four questions above point the same way, that is your machine.
Frequently Asked Questions
What is the difference between horizontal and vertical broaching?
The difference is the direction of the cutting stroke. A horizontal broaching machine drives the broach along a level bed, parallel to the floor; a vertical broaching machine drives it up or down an upright column. Cut quality is comparable in both layouts — the practical consequences are stroke length, floor space, chip removal, and how parts load.
Which is better, horizontal or vertical broaching?
Neither is better overall — each wins on specific work. Choose horizontal for long strokes, large heavy workpieces that load from above, and in-line conveyor flow. Choose vertical for small and mid-size parts, tight floor space, cleanliness needs in difficult materials, and overlapping-cycle automation. Many plants run both, each assigned to the parts it handles best.
Why are most broaching machines vertical?
Because the vertical layout solves three everyday production problems at once. It grows upward, delivering a useful stroke in a compact footprint. Gravity pulls chips and coolant out of the cut without elaborate flushing. And parts load at a convenient station height, which suits both operators and automated feeders. For the majority of parts — gears, hubs, fittings — those advantages compound.
What is a linear broaching machine?
A linear broaching machine cuts by moving a multi-tooth broach in a straight line through or across the workpiece, completing the feature in one pass. Both horizontal and vertical broaching machines are linear machines — the label describes the cutting motion, not the orientation. The alternative is rotary broaching, which spins and wobbles a form tool on a lathe or screw machine.
The Bottom Line
Horizontal and vertical broaching machines are not competitors — they are the same process pointed in two directions. The difference between horizontal and vertical broaching machine layouts comes down to the part: heavy and long parts with deep features belong on the horizontal bed; compact parts, tight floors, and automated cells belong on the vertical column. When the answers conflict, weight the part first, stroke second, floor third, and flow fourth. And when you are ready to compare actual machines, contact BroachingMach — as a broaching machine manufacturer we build both configurations and can recommend the right one for your parts, volumes, and building.
References
- Vertical broaching machine — US5833411A — Forst Technologie, 1998; vertical broaching machine architecture: machine stand with upper rail, lifting carriage driven by lifting spindles, workpiece holder mounted on the rail for pull and compressive broaching jobs.
- Vertical broaching machine — US3960056A — US3960056A, 1976; pull-up internal broaching: workpiece holder on the machining table, broach slide mounted beneath the table drawing the broach through the workpiece.
- Vertical internal push broaching machine — US6409442B1 — US6409442B1, 1999; push-type internal broaching: machine column, workpiece lifting table on carriage guideways, feeder carriage beneath the lifting table.